Start with the risk level of the pack
Security planning begins with the product itself. A carton for high-value consumer goods needs a different setup to a pack for temperature-sensitive foods or a batch that moves through several depots before it reaches the shelf. We look at where loss can happen, how the pack is handled, and whether the main concern is counterfeiting, tampering, diversion or product mix-ups.
For South African converters, the practical questions matter. Will the pack sit in humid Durban air, move through a cold store in Gauteng, or spend days in a container near the coast? Those conditions affect ink choice, drying time and adhesion, so the plan must work on press and in real transport conditions.
Use overt, covert and coded layers together
A single security feature is rarely enough on its own. A stronger pack usually combines visible cues for the customer, hidden checks for inspectors, and coded markers for traceability. That mix makes copying harder and gives your team more than one way to verify the pack.
- Overt features are visible changes, such as colour-shift or temperature response on the printed pack.
- Covert features are hidden checks that need a defined method to read them, such as a specific viewing setup or test step.
- Coded features link the pack to a batch, site, or product range for internal tracking and verification.
The right balance depends on who must check the pack first, a consumer, a warehouse team, or a quality inspector. We help define that order so the system is useful, not just decorative.
Set the trigger points and the reader method
Security only works if the trigger is clear. If an ink changes colour at the wrong temperature, it can confuse operators and create complaints. If a covert feature needs a special light or filter, that method must be practical for the site and not expensive to repeat.
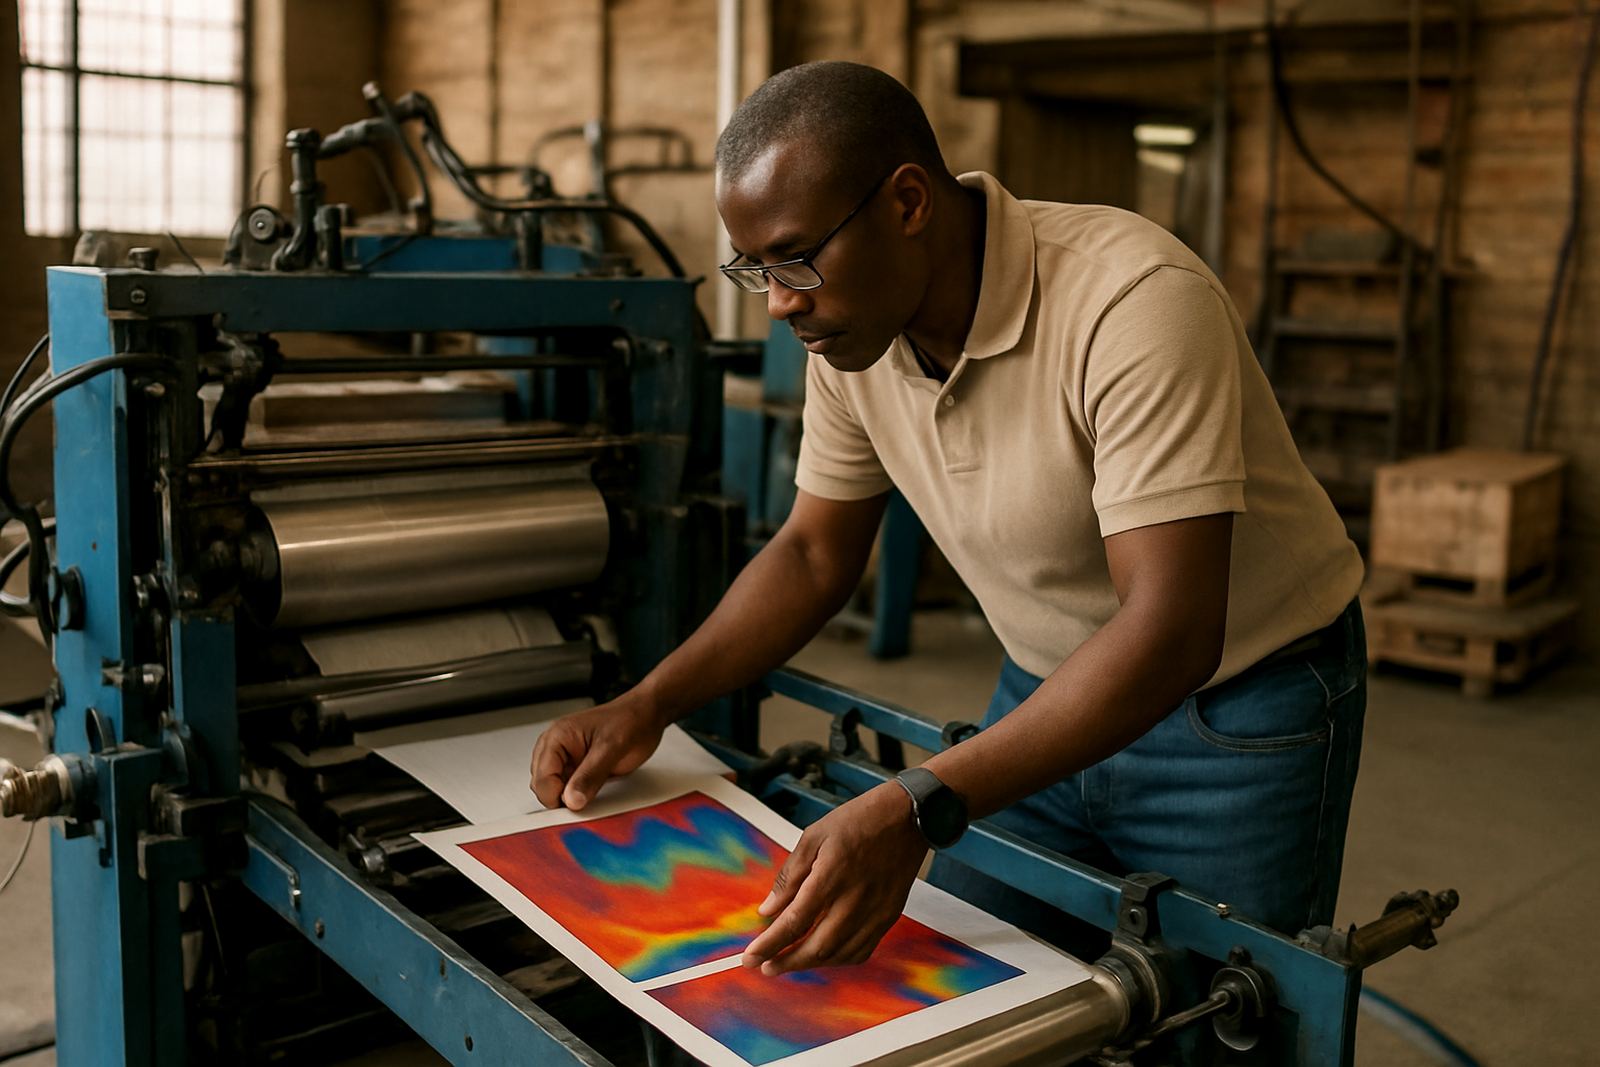
We build the plan around measurable points. For thermochromic work, that may include a colour change at a chosen threshold. For security features, it may include a coded pattern, a verification setup, or a simple test step that quality control can repeat without delay.
- Choose the event you want to signal, such as heat exposure or tamper risk.
- Define who must see it and where they will check it.
- Confirm how it will be read on the line and in the field.
- Record the approved method for future batches and audits.
Match the ink to the carton, label or sleeve
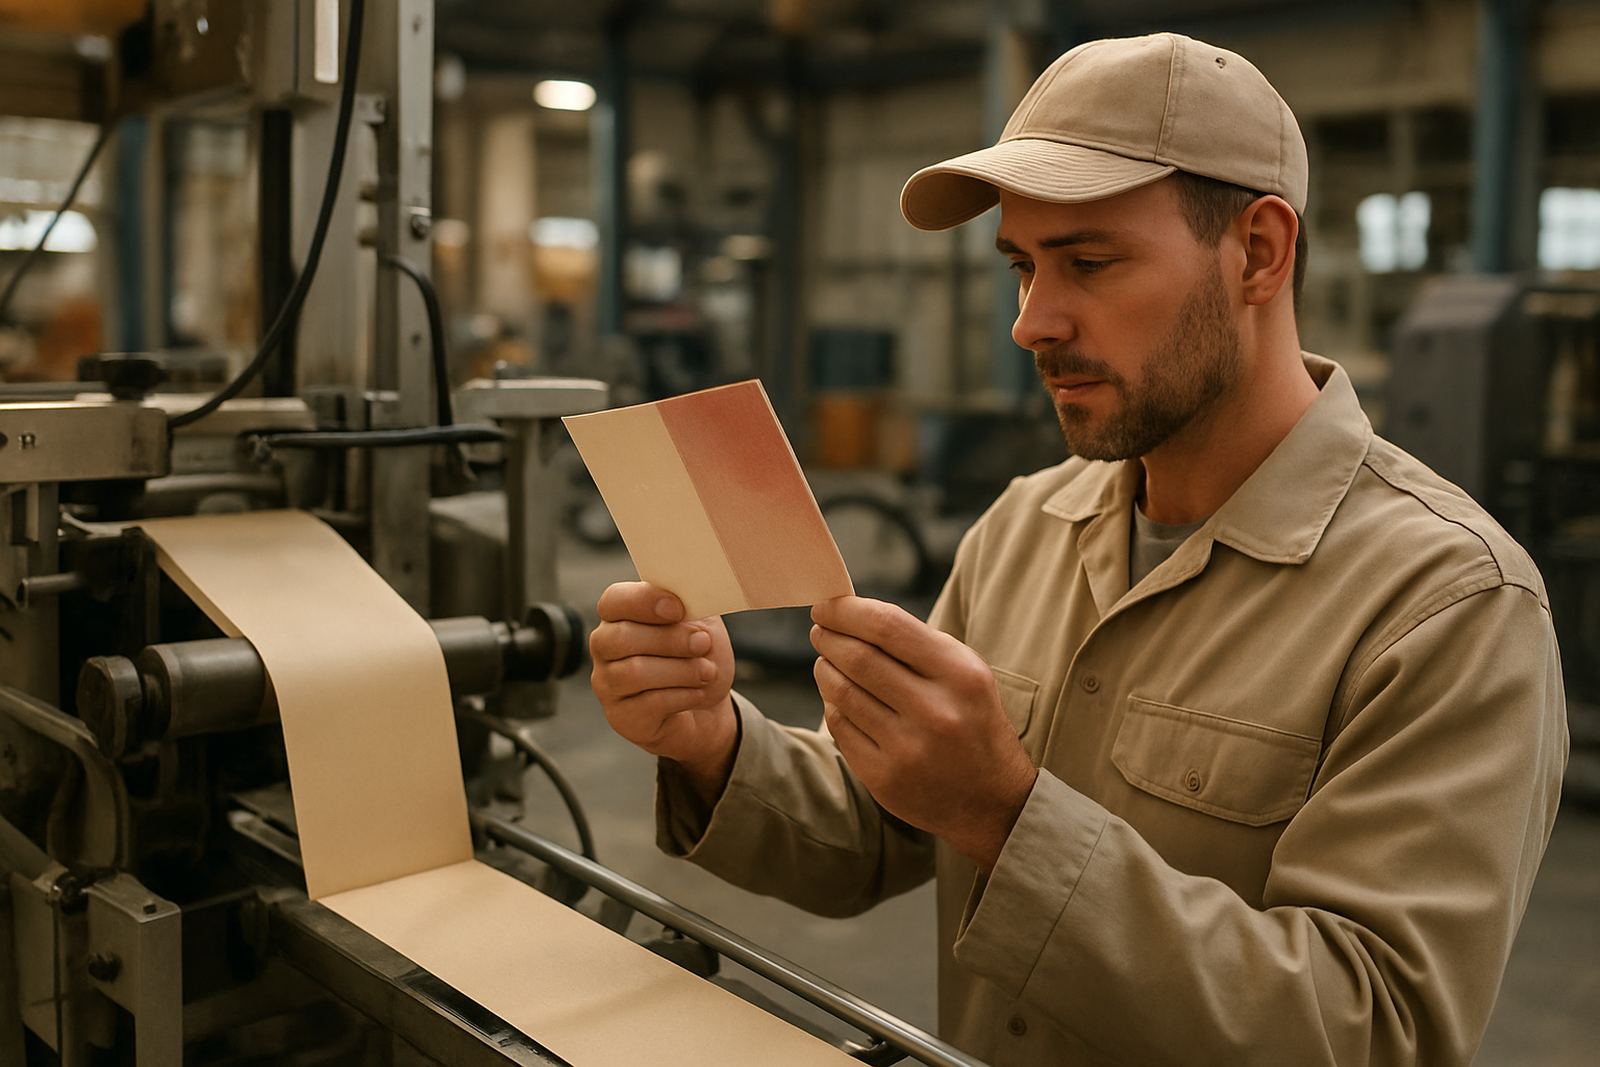
Not every substrate behaves the same. A coated carton, a shrink sleeve and a plain paper label all take ink differently. Adhesion, drying and rub resistance can change a lot between a sample that looks good in the lab and a pack that goes through folding, gluing or high-speed packing.
That is why we carry out drawdown panels, coating compatibility checks and adhesion tests before a full run. For higher-risk packaging, this step is worth the time because it reduces the chance of poor holdout, scuffing or a feature that disappears too early in handling. If the line runs fast, we also check whether the ink settles well under production speed and whether the print stays legible after conversion.
Keep the security plan practical for the plant
A security feature must survive the real plant environment. In Jacobs and along the coast, humidity can change the way inks behave. In colder inland plants, start-up conditions can affect cure and print stability. Load-shedding adds another layer because presses, dryers and inspection lights may come back online at different stages.
For that reason, planning should include what happens during a stop-start shift, who signs off the first good sheet after an interruption, and how retained samples are stored. Our batch retain library supports traceability, so approved references are kept for later comparison if a client queries a pack or a batch needs a recheck.
Build the approval trail before full production
Good security planning is not a one-step signoff. It should move from sample to trial to approved batch, with each stage recorded clearly. That makes it easier for a packaging converter to supply multiple customers, multiple SKUs, or several depots without losing control of the specification.
Our support process is straightforward and practical:
- Review the risk, substrate and print method.
- Prepare test panels and confirm the colour or trigger point.
- Run trial batch making and press startup support.
- Check rub resistance, UV response and adhesion.
- Lock the approved version into the batch record and retain sample file.
From our Jacobs base in Durban, we support converters nationwide, including Pinetown, Prospecton, Cape Town, Gqeberha, Johannesburg and Pretoria. That means the same planning approach can be used across different plants and pack lines, with local conditions taken into account.