Start with the pack requirement, not the ink sample
Every pack test should begin with the end use. A carton for chilled food in Durban needs different performance from a sachet, sleeve or label going into a dry warehouse in Johannesburg. Write down what the pack must do, then match the test to that job. If the item is cold-chain, note the target trigger temperature, how long the pack will sit in cold rooms and whether condensation is expected. If it is a security print, record where the feature must sit, who will inspect it and what the pass or fail cue looks like.
Set the substrate, coating, print process and drying method before you test. A good result on one paper stock means very little if the final order changes to a film or a heavier board. For specialised inks, the real question is not only whether the colour changes, but whether it does so at the right point and stays consistent across the batch.
- Confirm substrate type, weight and finish.
- Note the intended print process and drying or curing method.
- Record the pack use case, storage conditions and shelf life.
- Define the exact pass standard before the first drawdown panel.
Run drawdowns before press trials
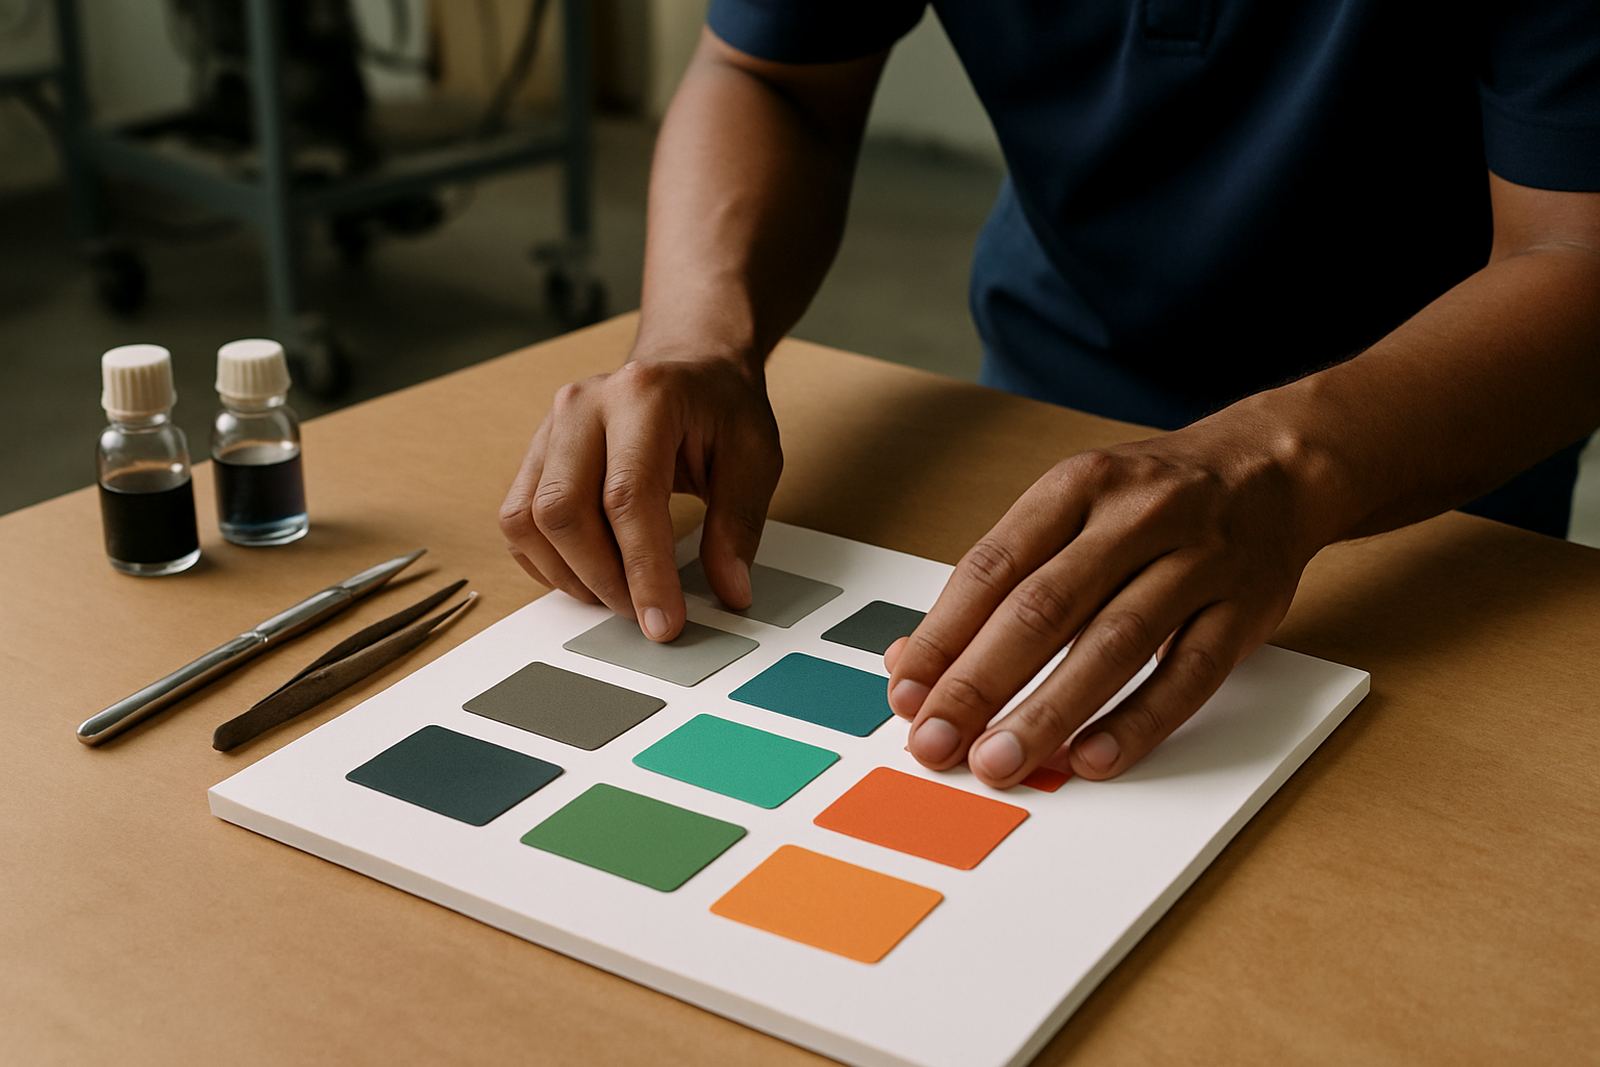
Drawdown panels give you a controlled starting point. They let you compare colour response, coverage and opacity before you commit press time. At this stage, check whether the ink sits cleanly on the substrate, whether there is misting or pinholing, and whether the intended effect appears at the right film thickness. A thin application can underperform, while a heavy coat can slow drying and affect packign line speed.
Where possible, prepare more than one drawdown level. That helps you see the threshold window and decide how much change is acceptable before the feature becomes too sensitive or too slow to respond. For thermochromic work, test the return to base colour as well. A feature that changes well but comes back slowly can confuse pack workers and end users.
- Make at least three drawdowns at different coat weights.
- Check the base colour, trigger point and return rate.
- Inspect for streaks, pinholes, poor laydown and edge lift.
- Keep one retained panel for later comparison against live production.
Test adhesion, rub resistance and coating compatibility
Once the ink looks right, it must survive handling. Adhesion testing tells you whether the ink bonds properly to the substrate or topcoat. Rub resistance checks whether the print will scuff in transit, during packing or on retail display. Coating compatibility is just as important. Some varnishes and laminations can dull the effect, weaken the trigger or interfere with security features.
Use the same drying window that the production line will use, then test after the pack has rested. Immediate results can be misleading. A print that seems fine at 10 minutes may fail after 24 hours, especially in humid coastal conditions around Durban or Port Elizabeth. If the packs will go through cold storage, test after temperature cycling too. Moisture can shift the finish, and the fault only shows up after the first chill cycle.
- Run tape pull or cross-hatch adhesion checks where suitable.
- Do dry rub and wet rub checks using the expected handling pressure.
- Test after 24 hours, not only straight after drying.
- Confirm whether the overprint varnish or laminate affects the feature.
Verify the trigger point on the actual packaging line
Thermochromic inks must change at the right moment, not just somewhere near it. That means checking the trigger temperature against your actual process and storage conditions. A pack that responds too early may give false signals in transit. One that responds too late may miss the point entirely. Check the trigger while the pack is on the line, in the packing hall and after storage if the product is sensitive to heat or cold.
Keep the test conditions practical. Use the same trays, cartons or wrappers that the customer will use. If the item moves from a hot filling area into a cooler store room, allow for the swing in temperature. For products sent nationwide, this matters a lot, because a delivery from Jacobs to Pretoria will face different daytime heat than a coastal route in winter. A good test should show repeatable behaviour in those real conditions.
- Measure the trigger point on full-size samples, not only lab strips.
- Test after exposure to heat, cold and humidity.
- Check how fast the colour returns once the pack cools or warms.
- Record any mismatch between target temperature and real line conditions.
Check security features under normal factory lighting
Security inks are only useful if they can be verified quickly by the right person. Test the feature under the lighting your warehouse, dispatch area and customer receiving bay actually use. UV verification setups should be checked in the same environment where the packs will be inspected, because glare, shade and distance all affect what the operator sees. A feature that is obvious in the lab can be hard to read on a noisy production floor.
Also test the print at the intended viewing angle and at the intended speed of inspection. If a feature depends on a hidden image, pattern shift or UV response, write down who will check it and what tool they will use. Keep the pass standard simple. Production teams need clear yes or no rules, not long notes that get lost during a busy shift.
- Confirm visibility under normal white light and UV light.
- Check the feature from the expected viewing distance.
- Train the checking team on the exact pass or fail cue.
- Retain a reference sample for every approved batch.
Build a trial batch record before sign-off
A trial batch is more than a sample run. It is the proof that the ink, substrate, process and handling method work together. Record the batch code, substrate lot, press settings, drying conditions and all test results. If there is a problem later, that record saves time and helps isolate whether the issue came from the ink, the coating or the press setup. It also helps with repeat orders, which is important when multiple sites are involved, from Pinetown to Cape Town.
Use a simple approval pack with three items: the approved sample, the retained batch sample and the test sheet. Keep these in a known place so production can compare them later. When the line restarts after a stoppage or load-shedding event, this record helps the team get back to spec faster. It also reduces waste, which matters when converters are trying to keep costs under control and meet customer deadlines.
- Keep one approved sample and one retained control sample.
- File all test results with batch number and date.
- Note press settings and any changes made during the trial.
- Sign off only when the pack passes every agreed test.
When to bring in technical support
Some issues show up only after the first live trial, especially if a customer changes the coating, substrate or line speed at the last minute. If the colour shift is weak, the adhesion is patchy or the security cue is too hard to read, get technical support before the next run. The goal is to adjust the formula or process early, not to carry the problem into full production.
At ThermoInk, our team works with packaging converters across Durban and nationwide on colour matching, threshold tuning, adhesion tests, rub resistance checks, UV verification setups and press startup support. That practical support can shorten approval time and help avoid repeat rework. If you need a pack test plan tailored to a specific substrate or product type, start with your sample details and the conditions the pack must survive.