What the freezer box brief called for
The client was a packaging converter in Durban supplying cartons for frozen food distribution into the inland and coastal markets. Their boxes were moving through cold stores, loading bays and retail back-of-house areas, so the print had to do more than look good on day one. It needed to stay readable after stacking, wrap film contact and repeated handling in cold, sometimes damp conditions.
The brief was simple in wording but exacting in practice: make the box carry a clear temperature cue, protect the printed area from rub wear, and keep the overall finish suited to food packaging. The client also wanted a clean security element that would help with authenticity checks if packs were diverted or mixed in transit.
- Project type: freezer box print development
- Client location: Durban, with distribution into KwaZulu-Natal and beyond
- Main challenge: low-temperature visibility plus scuff resistance
- Print environment: high-volume carton conversion and folding lines
Cold room conditions and press line limits
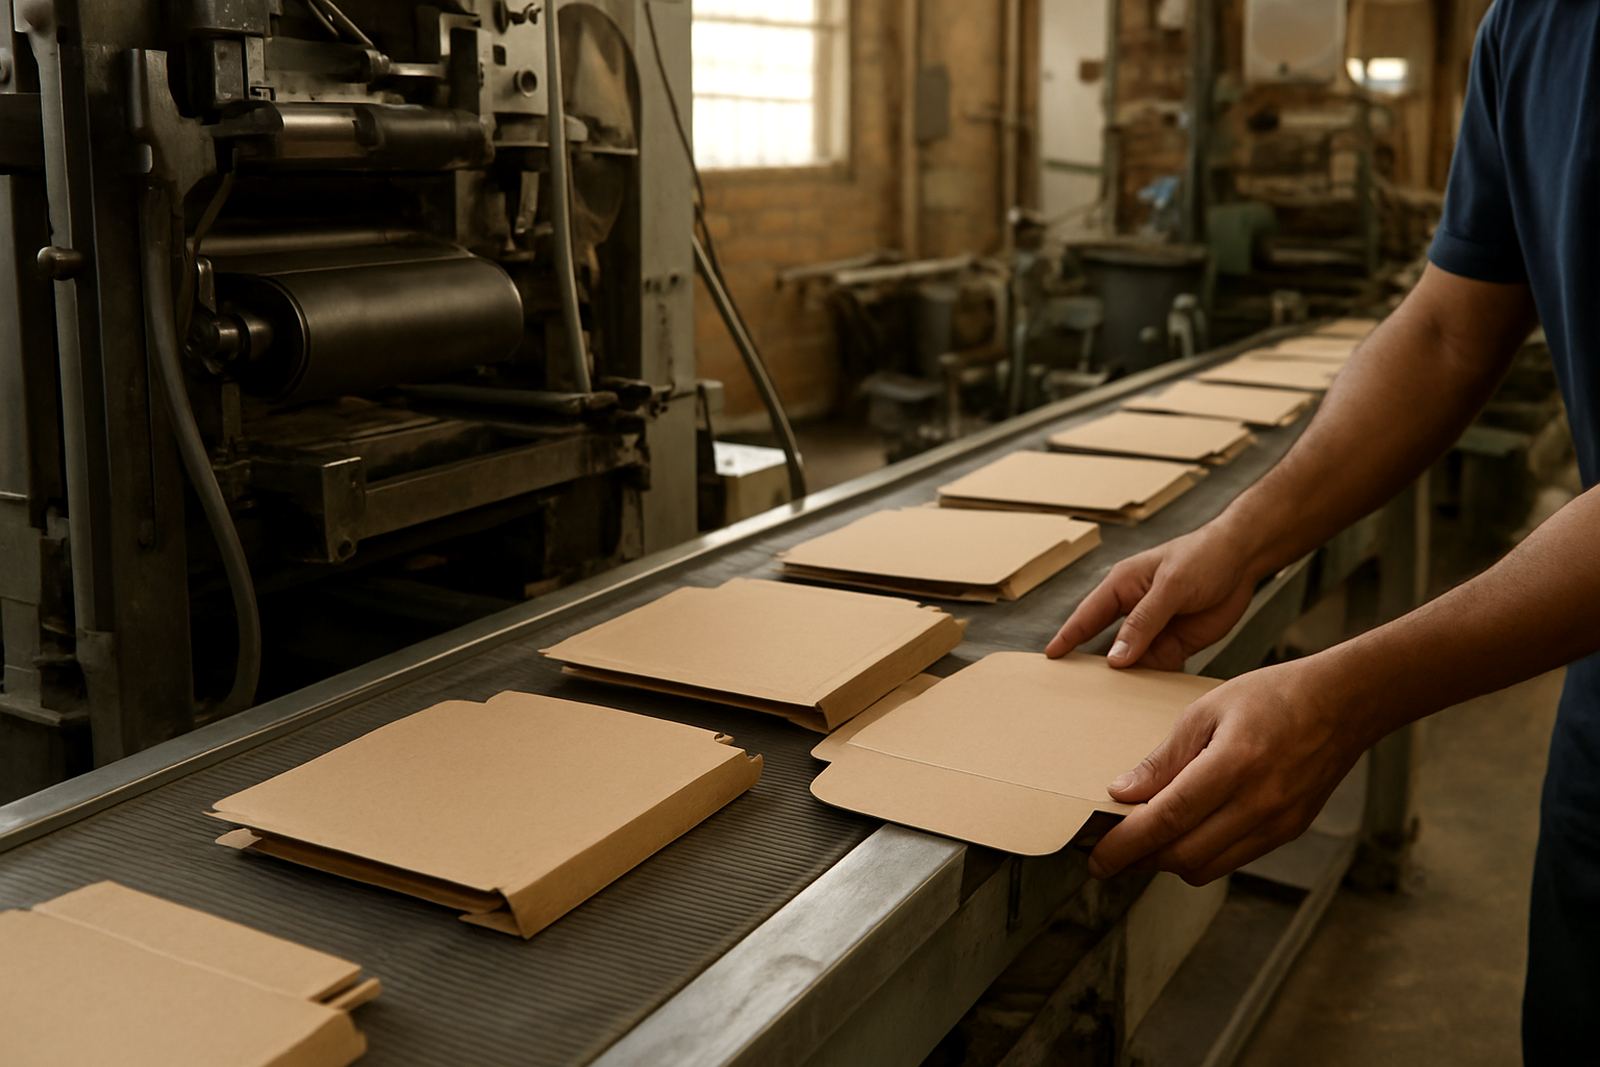
We started with the realities of the box itself. These cartons would see chilled handling, condensation and repeated movement against other packs, so a standard ink approach would not be enough. The print had to keep its colour-changing cue visible at the right temperature band, while staying stable through die-cutting, folding and glueing.
Another constraint was the pace of production. The converter could not afford long stoppages for trial after trial, especially with export and national dispatch windows on the same week. We worked within a tight approval cycle and kept the first sample set close to the machine settings they already used.
- Target temperature cue: visible shift in the low temperature band used for freezer packing
- Format: carton panels and selected warning or indicator zones
- Key resistance goal: rub resistance during stacking and transit
- Production note: press-friendly application with no major line changes
What we supplied for the trial batch
The first stage was colour matching and threshold tuning. We prepared drawdown panels so the client could compare the thermochromic response at different temperatures before going onto the press. Nomfundo Khumalo led the colour lab work, while Shaun October handled technical sales support and press-facing guidance.
We also built a small trial batch for press startup support, then checked adhesion and rub resistance on cured samples. Pieter van Wyk set up the security ink component so the package carried a discreet authenticity mark, not something that shouted on the shelf but still gave a useful control point for the client’s internal checks.
- Colour matching against the client’s carton artwork
- Threshold tuning for the low-temp response band
- Adhesion tests on printed board samples
- Rub resistance checks after handling and stacking simulation
- Security pattern design for verification on select carton areas
Three weeks from sample to press approval
The work moved in three weeks from first sample discussion to approved production settings. Week one covered brief refinement, board review and the first drawdowns. Week two was trial batch making, with press startup support at the converter’s site and quick changes to the ink laydown where needed. Week three was final sign-off, retain samples and dispatch planning.
Jason Pillay coordinated the logistics so the samples reached the right people in time, while Lindokuhle Dlamini stayed close to the production side and sorted any run-time questions. The point was to keep the process practical, not overcomplicate it.
- Week 1: brief, substrate review and sample drawdowns
- Week 2: trial batch and press startup support
- Week 3: final approval, batch retain library entry and rollout plan
- Support area: Durban base with deliveries nationwide
Results on the finished cartons
Once the approved mix was running, the cartons gave a stronger visual cue in chilled conditions and held up better against rub during packing and transport. The security feature added another layer of control for the client, especially where stock moved between depots and third-party cold storage. The result was a freezer box print that did its job without adding unnecessary steps to the line.
The client also valued the practical side: less rejected stock, clearer pack identification and better confidence that the cartons would still look correct by the time they reached the store room. In a cold chain enviroment, that matters more than a flashy finish.
- Better low-temperature visibility at point of use
- Improved rub resistance during handling and pallet movement
- Cleaner security verification for internal checks
- Less rework from early print wear
What we would repeat on the next freezer pack job
If we were repeating this job for another frozen food carton, we would keep the same sequence: sample first, threshold tuning second, then a controlled trial batch before release. That order saves time and avoids chasing issues after full production starts.
We would also keep batch retan samples, because freezer pack work often needs a reference later when artwork changes or the board changes supplier. For Durban converters, and for sites in Pinetown, Prospecton or farther afield, that kind of control makes day-to-day production easier.
- Start with drawdown panels, not a full press run
- Keep a retain library for each approved batch
- Recheck adhesion if the board or coating changes
- Retest after any major temperature or humidity shift
If your carton needs a temperature cue, a security mark or better scuff resistance, we can set up the sample work and guide the press checks from Jacobs to the rest of the country.
Key facts
| Project | Newlands Frozen Boxes |
|---|---|
| Client type | Packaging converter supplying freezer cartons |
| Location | Durban, KwaZulu-Natal |
| Timeline | 3 weeks from brief to approval |
| Core technologies | Thermochromic ink and security ink |
| Key tests | Adhesion, rub resistance, UV verification and press startup checks |